
Bold, long-lasting prints for team shirts, hoodies and fan wear, produced in-house with color-matched inks.
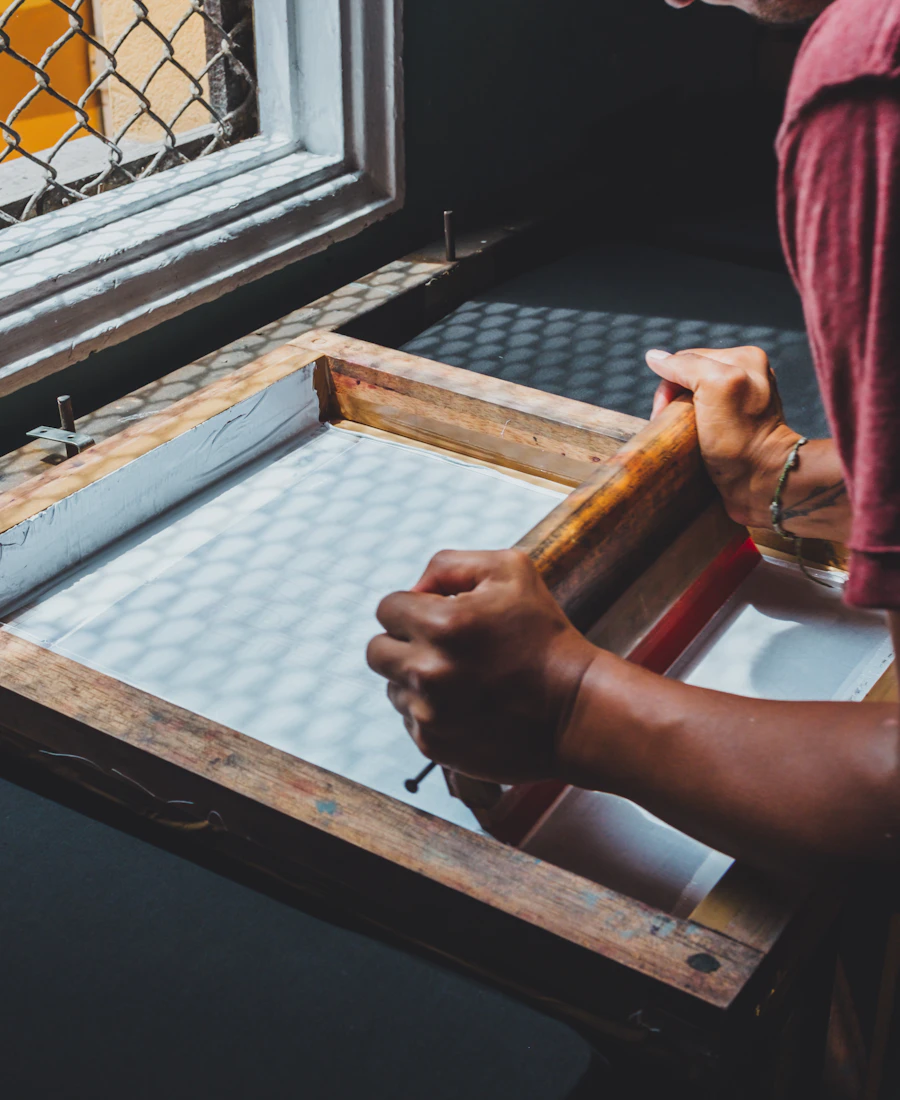
Screen printing is the go-to choice for strong, vibrant logos and graphics, especially on larger runs. Your artwork is separated into colors, and each color gets its own screen for sharp, accurate results.
We choose the right ink for your fabric: soft water-based inks for a light feel, or plastisol for bright, opaque colors on dark garments. Every print is heat-cured so it stays put through washing and wear.
Eight controlled stages give clean, durable prints on every piece.
Your design is split into individual color layers, each printed with its own screen.
Mesh screens are coated with emulsion and the design is exposed with UV light.
Inks are mixed to your brand colors and chosen to suit the fabric.
Screens are mounted and aligned on the press so every color lands in the right place.
Ink is pushed through the screen by squeegee, by hand for samples or on automatic presses for bulk.
Printed pieces pass through a heat dryer that bonds the ink to the fabric permanently.
Each print is checked for color, alignment and coverage before stitching.
Sample pieces are washed to confirm the print does not crack or fade.
Screen printing is ideal for bold logos, team names and numbers on larger quantities. For full-color, all-over designs we also offer sublimation, and for a premium textured look, embroidery.
Bright, opaque colors even on dark fabric.
Water-based inks for a light, breathable print.
Heat-cured prints made to survive many washes.
Send us your design, quantity and deadline. Our team replies with pricing and next steps within one working day.